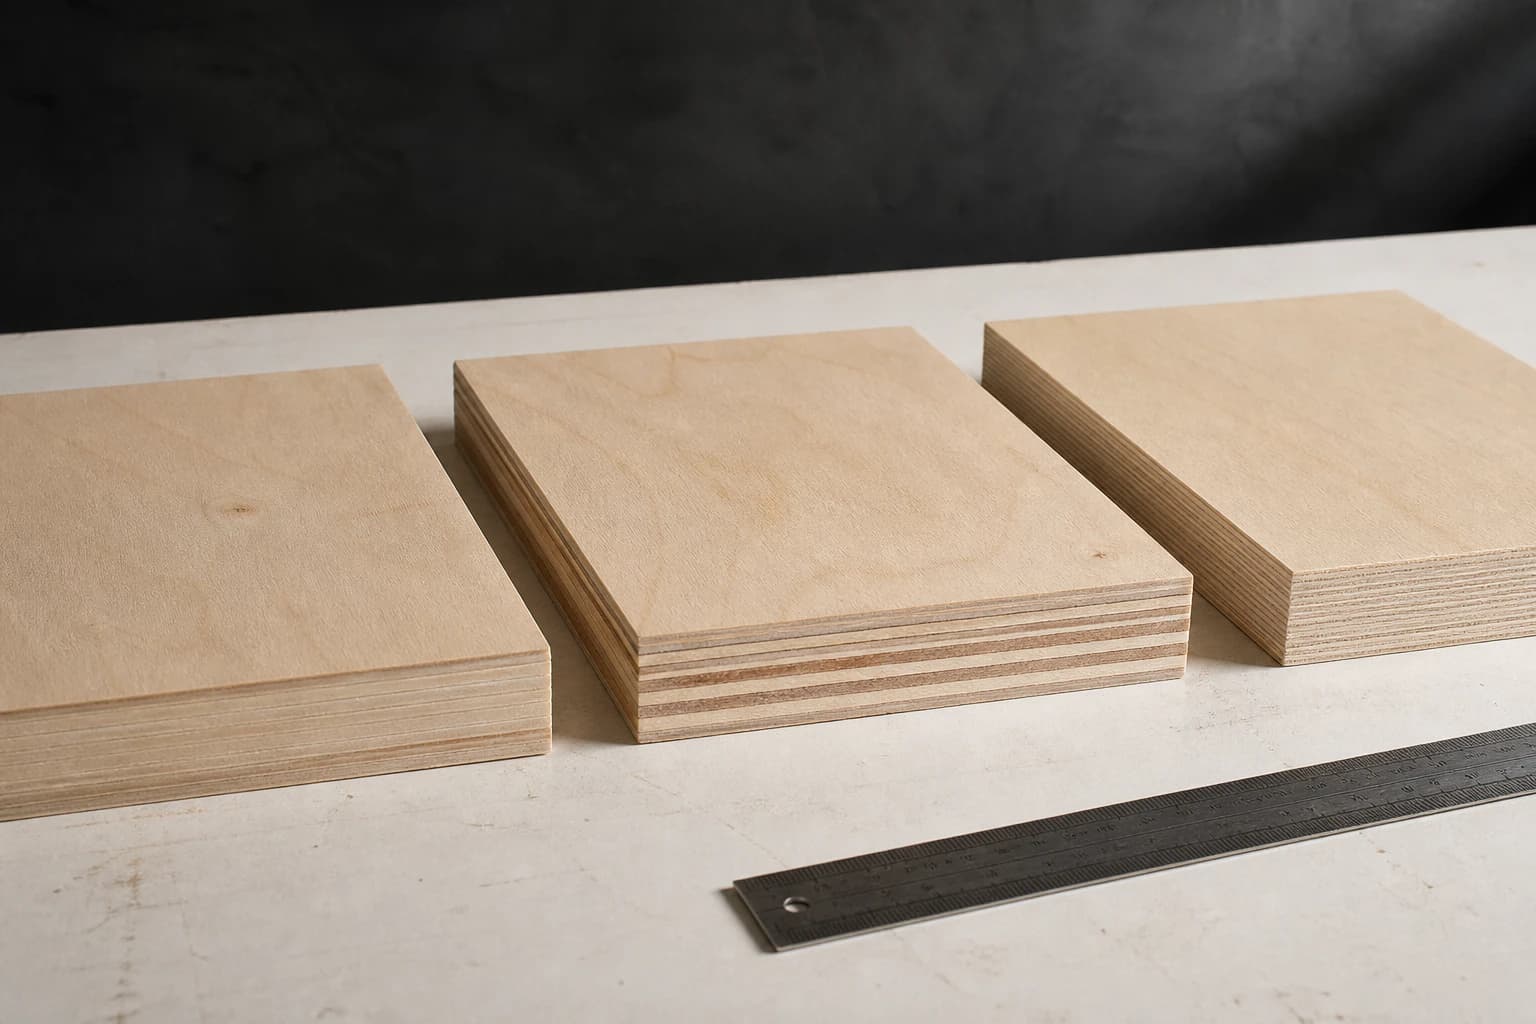
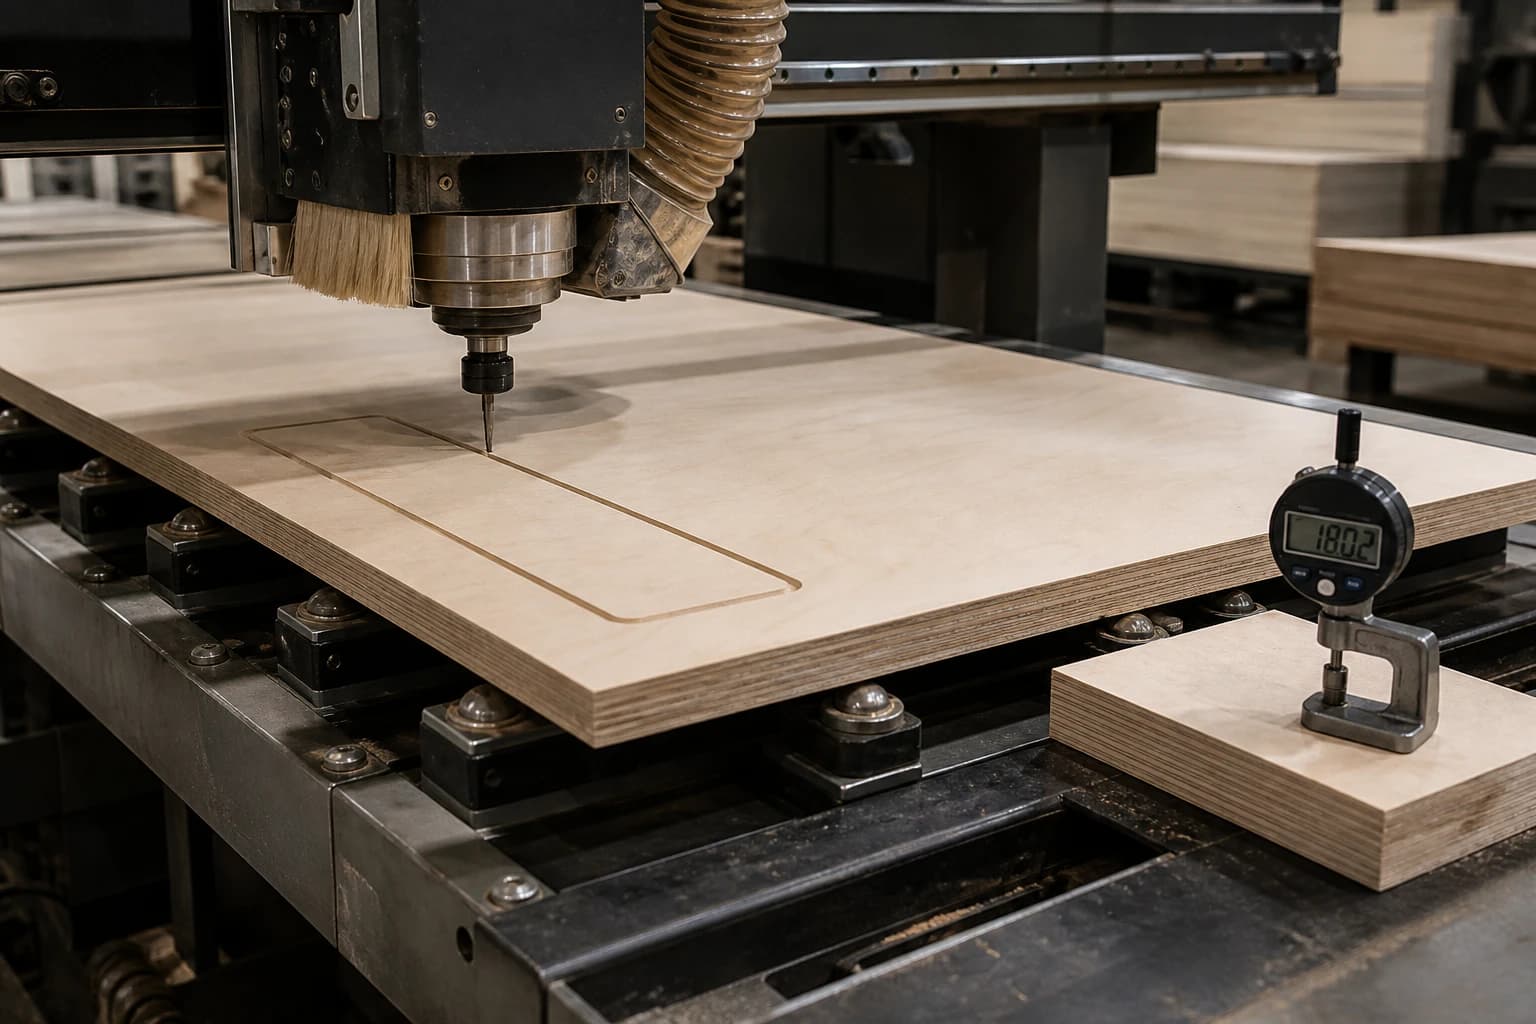
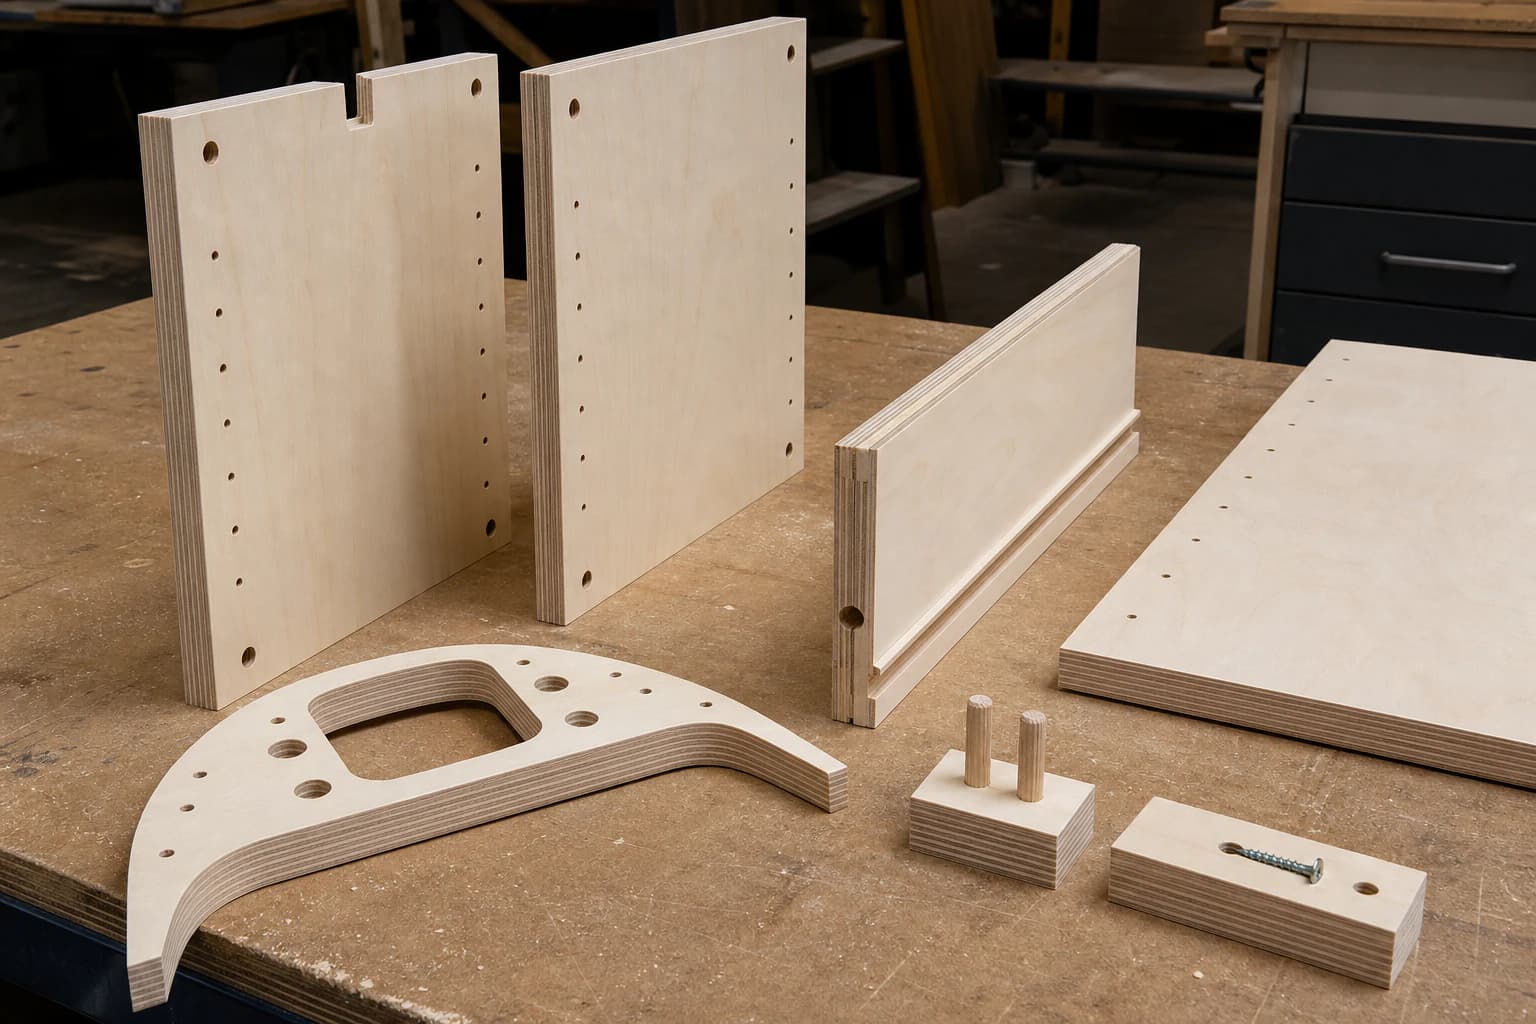
| Product construction | Birch face and utility birch back over a disclosed poplar or value-led combi core | Selected birch face/back over a calibrated combi, hardwood, eucalyptus or selected-birch export core | Selected birch face/back over an all-birch or buyer-approved precision core |
|---|
| Face veneer species | Natural birch face veneer; species reference recorded in the order | Selected birch face veneer matched to the finishing option | Selected birch face veneer frozen by approved appearance and supplier lot |
|---|
| Back veneer species | Utility birch back veneer with grade scope stated | Birch back veneer selected with the face/core balance | Selected birch back veneer held to the approved sample and machining programme |
|---|
| Face / back grade reference | C/D, BB/CP or buyer sample with face and back named separately | BB/CP or BB/BB reference with supplier grade mapping | B/BB, BB/BB or approved selected reference with repair limits |
|---|
| Face veneer thickness / reference | Order-defined supplier construction value; no fixed millimetre value is assumed | CUZI PLY construction sheet and approved sample record the face veneer reference | Face veneer construction value is frozen with the precision sample and lot revision |
|---|
| Core species | Poplar or value-led combi | Combi, hardwood, eucalyptus or selected birch | All-birch or precision buyer-approved construction |
|---|
| Core construction | Calibrated veneer core with disclosed species option | Balanced low-gap multi-ply build | High-ply, balanced, void-controlled build |
|---|
| Lay-up and ply schedule | Thickness-specific schedule recorded | Symmetry and species sequence approved | Ply count and sequence frozen in the sample file |
|---|
| Core gap / overlap control | Commercial limits by approved edge | Written gap and overlap limit | Tight visual and measurable limit for exposed-edge work |
|---|
| Repair scope | Grade-permitted face and inner-ply repairs | Repairs limited by sample and use | Selected face and edge repair rules frozen |
|---|
| bond specifications | Interior MR or exterior option as ordered | Interior or exterior phenolic option | bond specifications matched to the application and required documents |
|---|
| emission requirements | E1 target available on request | E1 / E0 or TSCA option by construction | Project emission requirements for the exact build |
|---|
| Panel grade | Furniture utility / buyer reference | Recurring export furniture and machining grade | Precision and exposed-edge programme |
|---|
| Standard formats | 1220×2440 / nominal 4×8; 1250×2500 mm | 1220×2440 / nominal 4×8; 1250×2500; 1525×1525 mm | 1220×2440 / nominal 4×8; 1250×2500; 1525×1525 mm |
|---|
| Project-size feasibility | Standard 1220×2440 and 1250×2500 mm formats | 1525×3050 mm made to order after construction and flatness confirmation | 1525×3050, 1220×3800 or 2100×2800 mm made to order after construction, handling and packing confirmation |
|---|
| Thickness range | 3, 4, 6, 9, 12, 15, 18, 24 and 25 mm options; other values by construction | 3, 4, 6, 9, 12, 15, 18, 24 and 25 mm options | 4–40 mm according to the selected high-ply construction |
|---|
| Thickness tolerance | Typically ±0.5 mm target | Typically ±0.3 mm target | Typically ±0.2–0.3 mm target after qualification |
|---|
| Length / width tolerance | EN 315 option or approved order value, measured on the named panel format | EN 315 option with the order tolerance and measuring points recorded | A tighter project value with an agreed measurement method, conditioning and first-production check |
|---|
| Squareness / edge straightness | EN 315 option or buyer-agreed acceptance measured separately from panel size | Order records squareness and edge-straightness limits with the inspection method | Precision option uses agreed measurable limits, inspection points and a lot report |
|---|
| Flatness acceptance | Approved sample after agreed conditioning, support spacing and measuring span | Lot sampling records conditioning, stacking state, measuring span and acceptance | Selected-panel flatness map and first-article acceptance under the project support condition |
|---|
| Moisture target | 8–12% | 8–12% | 8–12% |
|---|
| Density / panel weight | Construction-specific; typically 520–650 kg/m³ | Typically 600–720 kg/m³ | Typically 680–760 kg/m³ for all-birch option |
|---|
| Surface calibration | Core calibrated before face finishing | Recurring thickness calibration | Machining-lot calibration and measurement map |
|---|
| Sanding and finish readiness | Sanded for paint or overlay preparation | Fine sanded to approved face reference | Fine calibrated sanding for clear finish or precision overlay |
|---|
| Edge treatment | Raw edge or protection by order | Cut, sand and seal option | Precision edge machining and compatible seal option |
|---|
| CNC / cutting option | Cut-to-size after allowance review | CNC routing, nesting and drilling by file | Qualified tooling, compensation and first-article option |
|---|
| Drilling and fixing | Pilot and fixing trial recommended | Edge-distance and screw-holding trial | First-article hole, insert and edge checks |
|---|
| Inspection plan | Face, size, thickness and moisture sample | Face/core reference, tolerance and flatness sample | Lot map, edge review, machining first article and batch traceability |
|---|
| Approved sample | Face and core edge retained | Full construction and machining sample | Golden sample plus measurable construction revision |
|---|
| Applications | Carcasses, painted furniture, fixtures | Cabinetry, transport interiors, routed parts | Exposed-edge furniture, jigs and precision components |
|---|
| Target markets | Middle East, Central Asia, Latin America | Australia and all primary markets | Australia and project-led precision buyers |
|---|
| Certification target | E1 / bond documents on request | E0/E1, exterior bond, TSCA or chain-of-custody documents as specified | Project-specific test and transaction documents |
|---|
| Packaging | Wrapped pallet with face sheet | Moisture barrier, aligned supports and face protection | Batch-separated precision pack with edge and corner protection |
|---|
| MOQ | One production lot | One export pack or agreed mixed programme | Qualified production and machining lot |
|---|
| Loading quantity | Calculated from actual thickness and pack | Calculated after size/thickness mix | Calculated after project format, supports and payload review |
|---|
| Lead time | 25–35 days typical planning | 30–45 days typical planning | 40–60 days after material and machining qualification |
|---|
| Quotation unit | USD/m³ | USD/m³ | USD/m³ plus machining where applicable |
|---|
| Lot identity / change control | Face, back, core species, bond and lay-up version identified on the production lot | Reference sample, calibration option and construction version linked to each recurring lot | Face, core, bond, ply schedule, calibration and reference-sample version remain consistent with the written order |
|---|